
Quick answer
Do not assume APMT1135 and APMT1604 can use the same cutter pocket. They are different insert-size platforms. The cutter manufacturer’s approved insert and spare-part list decides the match. A shared APMT name, a similar photograph or the same cutter diameter is insufficient.
This guide is for replacing inserts in an existing cutter. If you are buying a new cutter and inserts together, request an approved assembly. Choosing the cheapest loose insert first and trying to fit a cutter around it creates an avoidable compatibility problem.
A manufacturer-specific dimension comparison
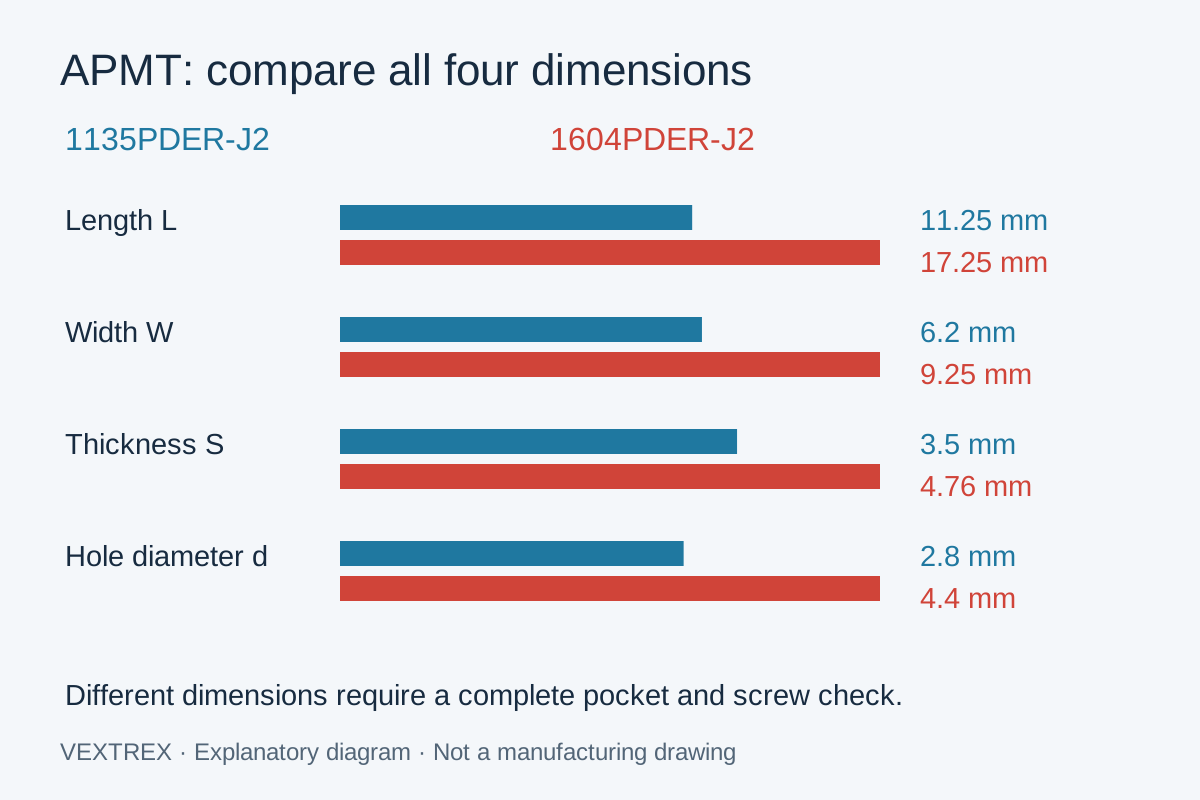
ECHAINTOOL’s official product table lists the following two J2 examples. All dimensions below are in millimetres and follow that manufacturer’s L, W, S, d and R labels. They are examples, not universal dimensions for every APMT product.
| Exact example code | L | W | S | d | R |
|---|---|---|---|---|---|
| APMT1135PDER-J2 | 11.25 | 6.2 | 3.5 | 2.8 | 0.8 |
| APMT1604PDER-J2 | 17.25 | 9.25 | 4.76 | 4.4 | 0.8 |
The shared 0.8 mm radius in this pair does not make the length, width, thickness or hole dimensions equal. These examples explain why a similar-looking top surface cannot establish interchangeability. Use the actual insert and cutter drawings when approving a replacement.
What must match the cutter?
- Approved insert platform: the exact designation permitted for that cutter model.
- Seat and support: how the insert contacts the pocket, including any manufacturer-specific seating features.
- Clamping parts: the screw, head, thread and tightening instructions specified for that assembly.
- Cutting position: how the insert locates the edge relative to the body and intended operation.
- Application: the approved material and operation for the proposed grade and geometry.
Treat these as questions to verify, not as a claim that any insert passing a visual inspection is safe to run. A screw entering a hole does not demonstrate correct seating. Stop if the insert rocks, leaves an unexplained gap, or requires modifying the pocket or screw.
If the cutter marking is unreadable
Send a photograph of the complete body, a close view of a clean empty pocket, the current insert from above and below, and the original packaging if available. Include cutter diameter, shank or mounting interface, number of pockets and the readable portions of any code. Label measurements as identification information, not confirmed manufacturing specifications.
Ask the supplier to return a candidate identification with the evidence used and the points still uncertain. If no reliable drawing or approved part list can be obtained, request a new matched cutter-and-insert assembly rather than accepting an unverified substitution for production.
Make the quote comparable
| Ask for | Why it belongs in the record |
|---|---|
| Full insert code, grade and chipbreaker | Prevents the platform name from hiding a different proposed product |
| Approved cutter model and spare-part codes | Identifies the assembly being checked |
| Workpiece material and operation | Separates a physical-fit check from application selection |
| Quantity, packing, destination and trial plan | Makes commercial offers and sample conditions comparable |
For example: “Existing cutter [full code], currently using [complete insert code]. Please confirm a compatible replacement for [material and operation], including grade, chipbreaker, approved screw and assembly instructions. Please identify any difference from the existing product before quotation.”
Browse APMT milling inserts and BAP400R cutter bodies. These are product-family entry points; confirm the exact pair before ordering. If the old grade is missing, use our replacement inquiry checklist.
Common questions
Can the same cutter diameter use either platform?
Different cutter designs can share an outside diameter. The pocket’s approved insert designation decides the match, not the diameter alone.
Does a larger insert automatically cut better?
No. Select the complete cutter system for the operation and machine. This size comparison provides no universal productivity ranking or cutting-data recommendation.
Manufacturer reference and scope
Table checked October 5, 2026, for the two named J2 examples. No equivalence with Vextrex’s eventual supplied grade or another manufacturer’s pocket is claimed. The identification and quotation checklists are Vextrex editorial guidance.
Need help confirming the exact tool specification?
Send the model code, clear tool photos, workpiece material and machining task. We will review compatibility and application details before confirming available options, price and lead time.