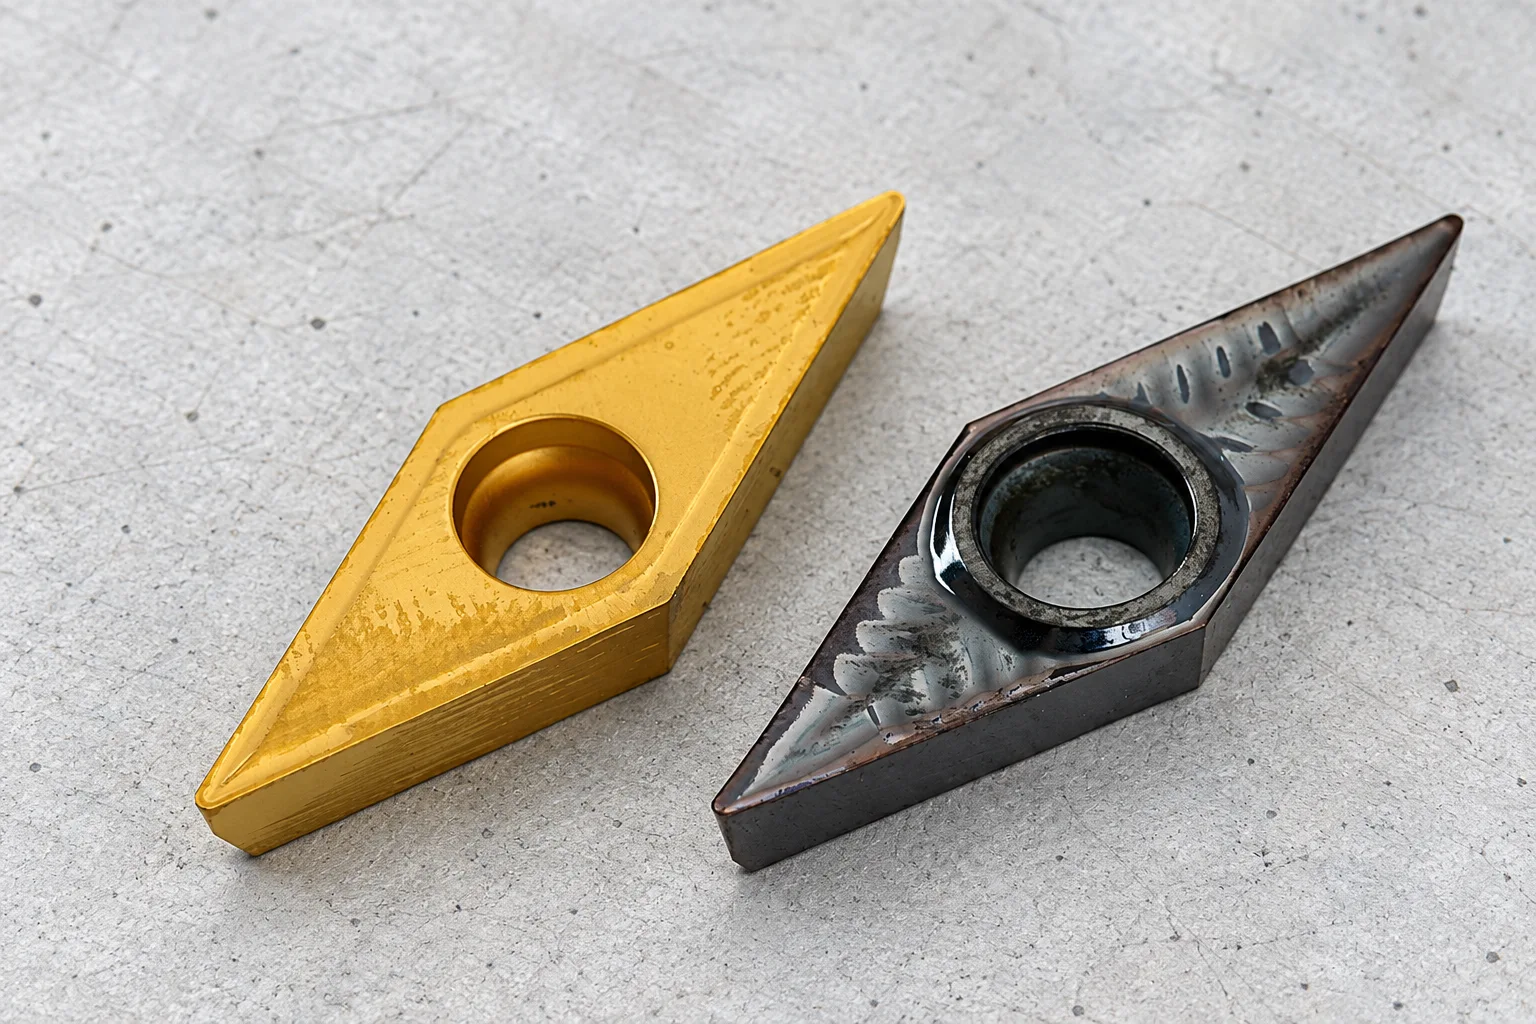

Choose DNMG when its 55-degree point and the complete holder can reach the required contour; consider VNMG’s narrower 35-degree point when the profile needs additional access. Neither shape is automatically the better finishing insert. A change of family also requires a compatible holder or approved cartridge.
For a buyer, the useful question is not “Which insert is sharper?” It is “Which complete tool can produce this drawing without interference, while keeping an appropriate cutting edge?” This guide separates profile access from dimensional fit so an enquiry does not become an expensive trial with the wrong seat.
What actually changes between DNMG and VNMG?
The first letter identifies the plan-view shape: D is a 55-degree rhombus and V is a 35-degree rhombus. Sandvik’s external-turning guidance identifies the D-style angle; Haas lists a 35-degree VNMG insert. These angles describe the insert outline, not the tool’s entering angle or its nose radius.
| Decision | DNMG | VNMG |
|---|---|---|
| Nominal point angle | 55 degrees | 35 degrees |
| Initial selection question | Can the broader point and holder reach the contour? | Is the narrower point needed for access? |
| Purchase check | Exact insert size, seat and clamp | Exact insert size, seat and clamp |
| What the family cannot confirm | Grade, chipbreaker suitability or finished surface | Grade, chipbreaker suitability or finished surface |
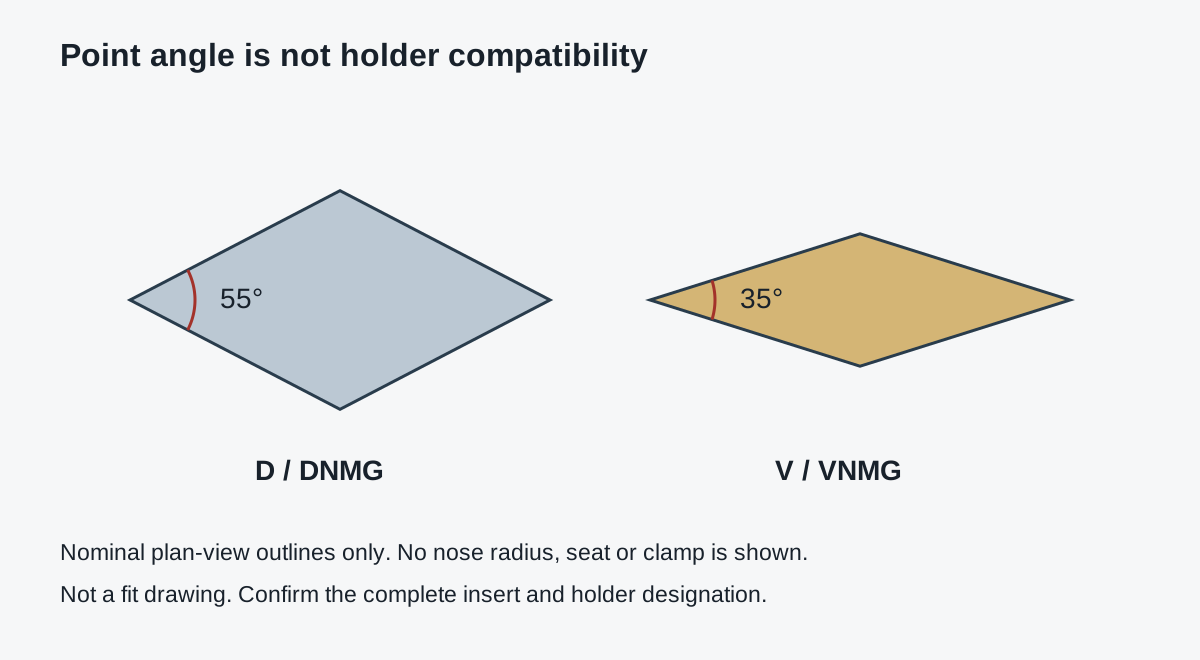
Sandvik advises balancing accessibility with edge strength and selecting the largest suitable point angle. Its insert-selection guide also treats nose radius, geometry and grade as separate decisions. A narrow point can solve an access problem while introducing a different edge-strength compromise; it is not a universal upgrade.
Check the drawing before changing the insert
Start with the feature that the current tool cannot produce. Mark the shoulder, taper, relief or reverse profile on a drawing. Include the approach and withdrawal moves, not only the final surface. Ask the programmer to review the complete tool envelope, including the holder body and clamp, against the workpiece, chuck and adjacent features.
Use this sequence for a quotation review:
- Identify whether the enquiry concerns an existing-tool replacement or a new profiling operation. These require different evidence.
- Highlight the inaccessible feature and provide the relevant section of the drawing, with confidential unrelated details removed if necessary.
- Send the complete holder code and photographs of its marking and seat. A photograph alone does not establish fit.
- Request the proposed insert and holder drawings together. Confirm the intended feed direction and tool orientation.
- Have the setup checked in the actual machine/programming workflow before approving a production trial.
This sequence is a purchasing review, not a collision-free toolpath guarantee. The insert point can clear a feature while another part of the assembly cannot.
Can a VNMG insert replace DNMG in the same holder?
Do not order it as a drop-in replacement. Different outlines require the seat and clamping arrangement to be checked against the holder manufacturer’s approved insert list. Matching a centre hole, apparent thickness or box size is insufficient. An insert that can be placed in a pocket has not thereby been shown to seat and clamp correctly.
Record the full codes rather than only “DNMG” and “VNMG.” Keep the insert packaging, holder marking and supplier drawing in the same enquiry. If the existing mark is unreadable, ask for identification before specifying a substitute. Do not modify a seat or shim to make an unapproved combination appear to fit.
The DNMG product page и VNMG product page are starting points for comparing available configurations. They do not replace written confirmation for your particular holder.
Keep the shape decision separate from the finish problem
If the complaint is a poor surface, ask where it occurs. Is the whole turned diameter affected, or only the profile transition? Does the issue follow a tool change, a material batch or a different setup? Gather that evidence before making shape the only variable.
A useful trial sheet records the workpiece specification, insert code, holder, tool projection, coolant arrangement, programmed conditions and inspection method. Change one selection variable at a time where practical. Agree the acceptance criterion before testing; do not infer a tool-life benefit from one satisfactory-looking part.
For code interpretation, use the separate turning-insert nomenclature guide. This article addresses profile access and holder fit, rather than repeating every position in the designation.
What should a buyer send for a meaningful quote?
Copy this checklist into the enquiry:
- Existing full insert code, including chipbreaker and grade, plus box-label photograph.
- Complete holder or cartridge code and seat photograph.
- Drawing extract showing the profile, radii, tolerances and finish requirement.
- Workpiece material specification and whether the cut is continuous or interrupted.
- Current process concern: access, chipping, finish, chip control or replacement supply.
- Trial quantity, expected recurring quantity and destination for the quotation.
Ask the supplier to distinguish an exact replacement from a proposed alternative. For an alternative, request a list of changed items and the technical basis for the recommendation. A quotation that changes holder, insert geometry and grade simultaneously should make those changes explicit.
Часто задаваемые вопросы
Does VNMG always give a better finish?
No. The narrower outline is principally a shape/access distinction. Judge a proposed finishing setup using the complete configuration and an agreed trial, rather than the family name alone.
Does the same nose radius make the inserts interchangeable?
No. Nose radius is only one feature. The complete outline, dimensions, seating and clamping must match the approved holder configuration.
Should I use VNMG for every undercut?
No. Some features require a dedicated grooving or other tool system. Ask for a complete tool-envelope review rather than assuming that a narrow point will clear the entire feature.
Request a configuration review
Send Vextrex your drawing extract, current holder code and full insert designation through the website enquiry form. Specify whether you need an exact replacement or a reviewed alternative. Configuration, grade, quantity and delivery terms should be confirmed in the quotation; this guide makes no machining-performance or stock guarantee.
Technical references and editorial scope
Manufacturer references checked 27 October 2026. Selection checklists and worksheets are editorial recommendations, not machining test reports. Named manufacturers are cited for technical reference; no endorsement or affiliation is implied.
Нужна помощь в подтверждении точной спецификации инструмента?
Отправьте код модели, четкие фотографии инструмента, материал заготовки и задачу обработки. Мы рассмотрим совместимость и детали приложения, прежде чем подтвердить доступные варианты, цену и время выполнения.