
A grooving insert’s cutting width must suit the groove, but width alone cannot establish whether the insert fits a holder. Confirm the complete insert designation, approved holder seat, cutting geometry and access limits before ordering. A 2 mm and a 3 mm insert are not automatically interchangeable.
“I need a 3 mm grooving insert” is a useful starting point, not a complete purchase specification. It leaves open whether the buyer wants an existing-tool replacement, a narrow finished groove, a wider groove made in several passes, or a parting operation. Resolve those differences before comparing prices.
Three dimensions that should not be confused
Keep the component groove, cutting edge and tool seat on separate lines in the enquiry. The groove drawing defines the required part feature. The insert drawing defines the cutting edge. The holder documentation establishes the supported insert configuration and tool access.
| Item to verify | What it answers | Evidence to request |
|---|---|---|
| Finished groove width and tolerance | What must the part contain? | Component drawing |
| Insert cutting width and corner radii | What edge profile is being purchased? | Exact insert drawing |
| Holder seat and clamping system | Is this insert approved for this tool? | Holder compatibility list/drawing |
| Required groove depth and location | Can the complete assembly reach it? | Part section and tool access drawing |
| Shank size, hand and mounting | Does the holder suit the actual setup? | Holder code and machine setup review |
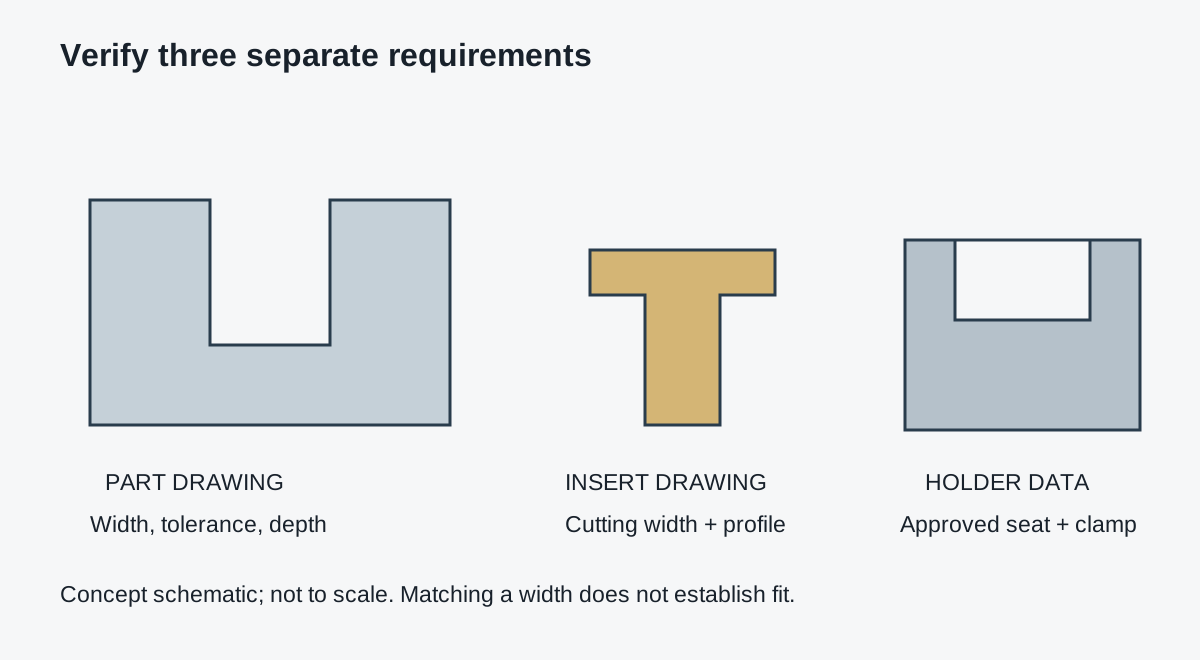
Do not infer cutting width from a supplier’s abbreviated model name alone. Ask which dimension the number represents and obtain the drawing for that exact item. Similar-looking codes from different catalogues should not be treated as a cross-brand fit guarantee.
First decide: replacement or new operation?
For a replacement, keep the existing holder fixed as a purchasing constraint. Send its complete marking, the insert box label, and clear photographs of the seat and clamping components. Request the same approved configuration or a documented alternative. If the supplied code differs, have the supplier explain the difference before an order is placed.
For a new operation, begin with the part drawing. State whether the groove is external, internal or on a face, and whether parting-off is also required. Do not assume a holder chosen for one approach is approved for another. Ask the supplier to review the full assembly rather than quote a loose insert in isolation.
This distinction also avoids an unhelpful price comparison: a loose replacement insert and a new matched holder-and-insert package solve different purchasing problems.
Can a narrower insert make a wider groove?
Sometimes, using an appropriate machining strategy. Sandvik’s external-grooving guide describes methods for grooves wider than the insert, including multiple grooving and plunge turning. That does not mean every insert is approved for sideways cutting or every holder can support the intended method.
For a wider groove, ask the process reviewer to identify the roughing method, finishing allowance, corner requirements and permitted feed directions. The buyer should purchase the configuration approved for that plan. Avoid changing to a wider cutting edge simply because its nominal width resembles the drawing; seat compatibility and access still need checking.
No generic speed, feed or lateral-cutting allowance is supplied here. Those recommendations need the exact tool system, material and operation.
Check depth, projection and chip space together
An insert can match the nominal groove width while the assembly still cannot reach the required depth. Request a section view showing the access restriction and the proposed tool projection. Distinguish a catalogue maximum for a specific configuration from the operating condition proposed for your part.
Sandvik’s parting-and-grooving setup guidance recommends short overhang to reduce vibration. Treat that as a setup consideration, not permission to shorten or alter a holder. Ask the responsible programmer/operator to confirm reach, clamping and coolant access for the selected arrangement.
For purchasing records, save the tool assembly drawing beside the part revision. If the groove depth or feature location changes later, flag the tool selection for review rather than assuming the original approval still covers the new part.
MGMN and MGEHR: order the specific combination
The Vextrex MGMN insert page y MGEHR holder page let buyers begin a configuration enquiry. A family label is not a universal interchangeability statement. The currently described holder option concerns 3 mm MGMN tooling; it should not be advertised as accepting every MGMN width.
Ask for confirmation of the exact insert-and-holder combination, including the seat, hand and shank. If you already own a holder, say so at the beginning. This prevents a supplier from proposing a complete new tool when the requirement is a replacement insert, or proposing a loose insert for an unidentified holder.
A quotation checklist that prevents repeat questions
- Part drawing revision, groove width/tolerance, corner radii, depth and feature location.
- External, internal, face-grooving or parting operation, including planned feed direction.
- Full existing insert and holder codes; attach legible photographs if available.
- Material specification and the specific production issue, if this is a replacement trial.
- Machine mounting constraints and who will approve the proposed tool assembly.
- Initial trial quantity, expected repeat quantity and delivery destination.
Ask the supplier to return a drawing reference, exact quoted designation and a clear statement of whether the holder is included. Keep alternatives as separate quotation lines. A lower unit price is not a saving if the quoted insert needs a different holder that was omitted from the comparison.
Preguntas frecuentes
Can I replace a 3 mm insert with a 2 mm one in my holder?
Only if the holder manufacturer explicitly approves that exact configuration. Do not infer fit from a similar body shape or the fact that an insert enters the seat.
Does insert width equal the finished groove tolerance?
No. A nominal width is not a completed-part acceptance result. Specify the part tolerance and agree how the proposed tool and process will be verified.
Is a grooving insert automatically suitable for parting off?
No. Have the supplier review the proposed operation, access and assembly rather than relying on the broad category name.
Get the fit checked before ordering
Usar el Vextrex enquiry form to send the groove drawing and complete holder code. Request a documented insert/holder match and identify any unresolved dimensions. Grade, availability, quantity and delivery terms remain subject to quotation confirmation.
Technical references and editorial scope
Manufacturer references checked 27 October 2026. Selection checklists and worksheets are editorial recommendations, not machining test reports. Named manufacturers are cited for technical reference; no endorsement or affiliation is implied.
¿Necesita ayuda para confirmar la especificación exacta de la herramienta?
Enviar el código modelo, fotos de herramientas claras, material de pieza y tarea de mecanizado. Revisaremos la compatibilidad y los detalles de la aplicación antes de confirmar las opciones disponibles, precio y tiempo de entrega.