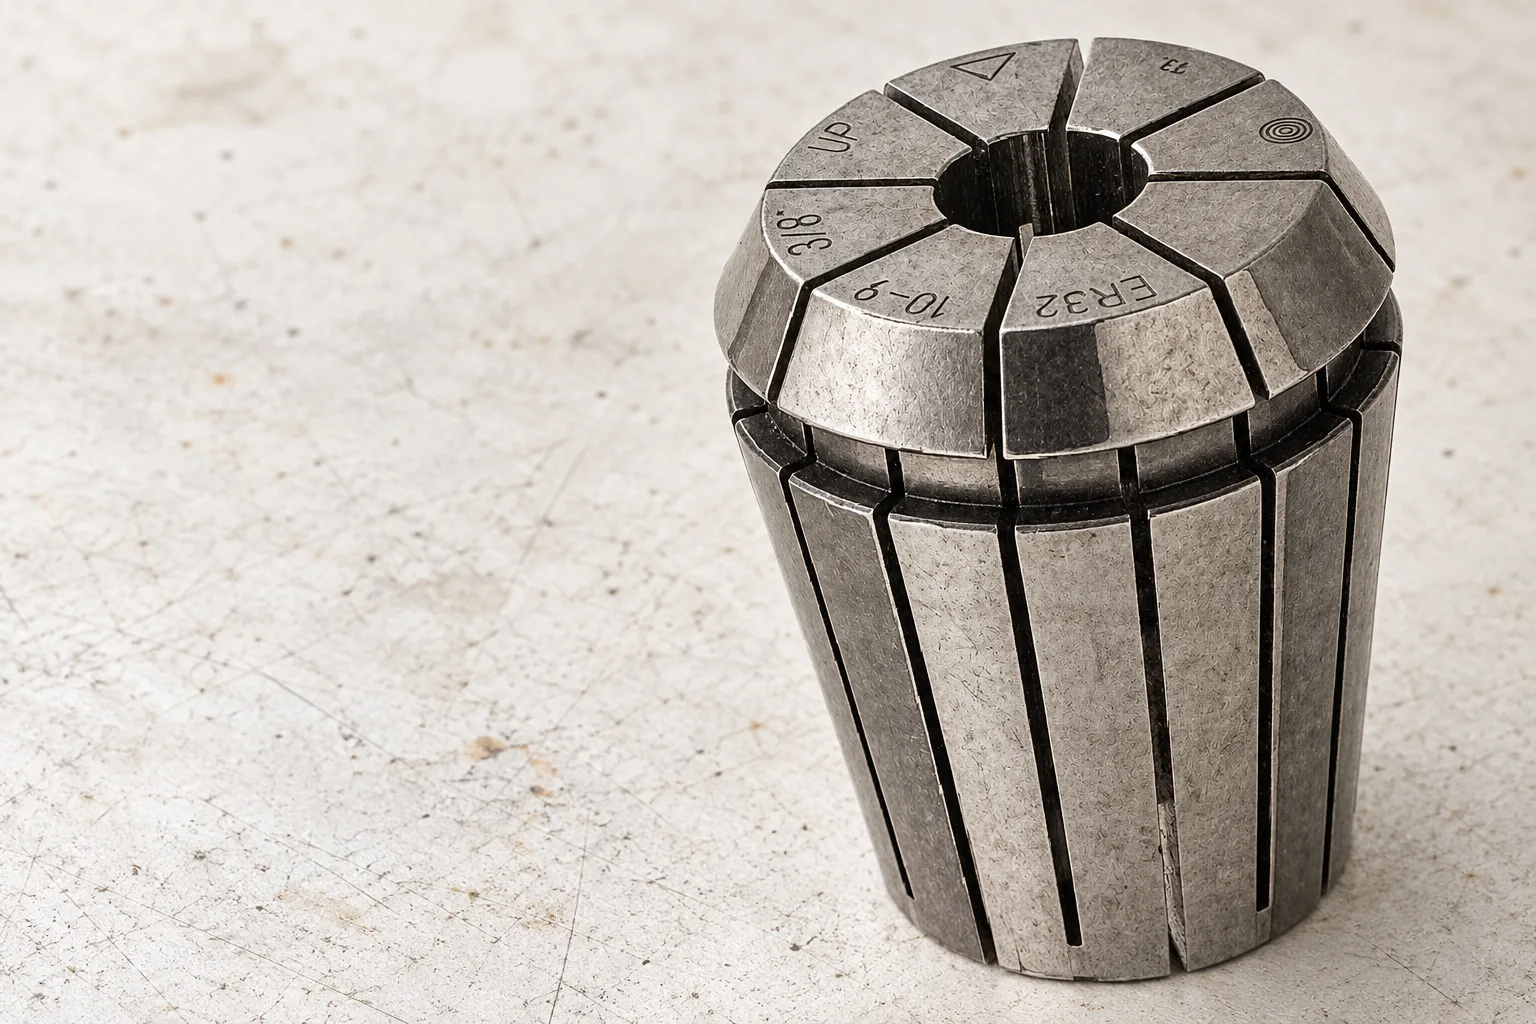

Do not blame the ER collet from a single runout reading. First confirm how the reading was taken, clean and correctly assemble the system, then compare controlled measurements while changing one component at a time. A collet specification and a complete spindle-mounted assembly measurement are not the same test.
For a purchasing team, a repeatable fault record is more useful than immediately ordering another cutter. It gives the tool supplier enough information to distinguish an assembly problem, a worn component and an unverified measurement. This guide provides that record; it does not supply a universal runout acceptance limit.
Define what the measurement actually describes
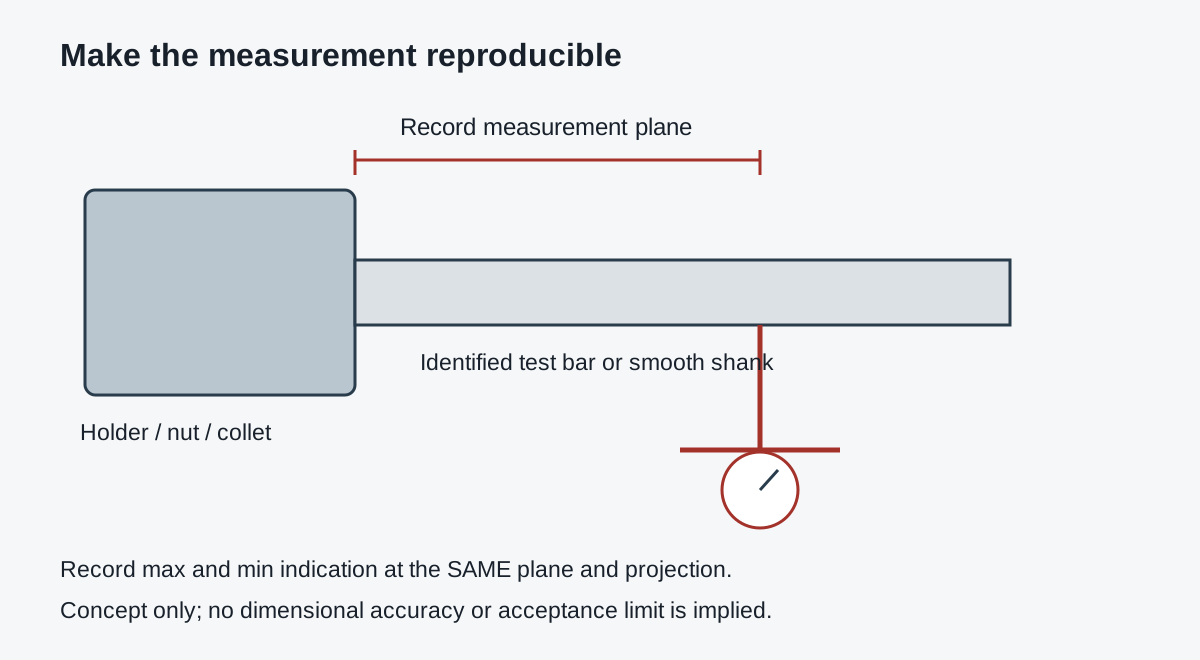
Record the test object and measurement location before comparing numbers. A reading taken on a ground test bar near the nut cannot simply be compared with a reading taken farther out on a cutting tool. Likewise, a supplier’s component certificate should be read with its stated test method and conditions.
| Record | Why the buyer needs it |
|---|---|
| Holder, nut and collet codes | Identifies the configuration being reviewed |
| Test bar/tool identity and shank diameter | Defines the object being measured |
| Measurement plane and projection | Makes subsequent readings comparable |
| Instrument, resolution and mounting | Records the measurement method |
| Maximum and minimum indication | Preserves the underlying observations |
| Assembly procedure and torque reference | Allows the setup to be reproduced |
Total indicated runout is the difference between the maximum and minimum readings over the specified rotation; Mitutoyo describes this max/min difference in its indicator documentation. For an arithmetic illustration only, readings of 0.012 mm and 0.004 mm give 0.008 mm. These are invented example readings to explain subtraction, not test results, a product claim or an acceptance threshold.
Clean and inspect before buying replacements
BIG DAISHOWA’s runout-control guidance identifies contamination as a source of assembly error. Check the accessible holder, collet, nut and tool-shank interfaces using the manufacturer’s cleaning instructions. Keep the observation factual: record what was found and whether the reading changed after correct reassembly.
Inspect for visible damage, corrosion or wear and refer suspect parts for competent assessment. Do not grind, polish or modify precision locating surfaces as an improvised correction. A component that looks cleaner is not automatically proven serviceable.
The separate maintenance guidance from BIG DAISHOWA discusses the nut/collet connection and holder condition. Do not overlook the nut when a fresh collet gives an unexpected result. Nor should a universal service life be inferred for all collets and nuts from one manufacturer’s test.
Verify assembly order and the actual torque reference
For its conventional ER system, REGO-FIX’s operating manual describes engaging the collet in the nut’s eccentric retaining ring before screwing the assembled nut onto the holder, and recommends a torque wrench. Follow the instructions for the actual equipment in use; a different retention system may have a different procedure.
Do not copy one torque figure into every ER32 job. The supplier’s torque table distinguishes nut types and clamping ranges. Match the reference to the exact components and required conditions. Keep the tool insertion and clamping-range requirements from the applicable manual with the setup sheet.
If the shank size is in doubt, resolve that first. The existing 6 mm versus quarter-inch collet guide addresses that separate sizing question. Runout troubleshooting cannot validate an unsuitable clamping range.
Make a controlled comparison, not a parts lottery
Have a competent operator perform checks under the machine and instrument manufacturers’ procedures, with powered spindle movement prevented during indicator contact. Never start the spindle with the indicator engaged. This article is a purchasing/diagnostic record, not a machine-specific service procedure.
After the baseline is recorded, agree the next comparison with the responsible technician. Where suitable approved reference components are available, change only the collet, only the nut, or only the test tool in each comparison. Keep projection, measurement plane and assembly method consistent. Stop and investigate if a component is damaged or the method cannot be reproduced.
| Comparison record | Hold constant | Change deliberately |
|---|---|---|
| Baseline after cleaning | Defined complete assembly and test method | No component substitution |
| Collet comparison | Approved holder, nut, test object and plane | Identified compatible collet |
| Nut comparison | Approved holder, collet, test object and plane | Identified compatible nut |
| Tool/test-bar comparison | Approved assembly and measurement method | Identified test object |
This worksheet helps isolate a question; it does not prove causation by itself. Preserve repeated results and ask the supplier to review inconsistent observations. If the concern appears to lie with the machine spindle or mounting interface, use qualified service support rather than continuing random consumable changes.
What should an ER collet or holder enquiry include?
Send a concise evidence pack: complete component codes, actual shank diameter, instrument details, measurement plane, projection, assembly/torque reference and recorded readings before and after cleaning. Include photographs that identify the parts and setup, with the machine safely stationary.
For a new purchase, specify the required accuracy together with the measurement conditions. Ask whether a quoted tolerance applies to the collet alone or the complete assembly, and request its test basis. State whether the quotation must include the holder, collet and nut or only one replacement item.
The BT40-ER32 toolholding page is a configuration enquiry starting point. Confirm spindle interface, pull stud, gauge length, collet range and nut before purchase; the ER32 label alone does not specify the whole tool assembly.
Preguntas frecuentes
Does a new collet guarantee low assembly runout?
No. It is only one component in the measurement chain. Review the holder, nut, tool, mounting and test method as well.
Is more tightening torque the solution?
Do not exceed the applicable manufacturer’s instructions to chase a smaller reading. Verify the correct reference and assembly before evaluating the result.
What runout limit should I put on my purchase order?
Use a requirement agreed for the application and state how it will be measured. This guide does not assign an unsupported universal tolerance to Vextrex products.
Request a documented configuration
Send the evidence pack through the Vextrex enquiry form. Ask for the proposed exact configuration and the basis for any accuracy claim. A controlled comparison and written requirement are more useful than ordering an unspecified “high-precision” collet.
Technical references and editorial scope
Manufacturer references checked 27 October 2026. Selection checklists and worksheets are editorial recommendations, not machining test reports. Named manufacturers are cited for technical reference; no endorsement or affiliation is implied.
¿Necesita ayuda para confirmar la especificación exacta de la herramienta?
Enviar el código modelo, fotos de herramientas claras, material de pieza y tarea de mecanizado. Revisaremos la compatibilidad y los detalles de la aplicación antes de confirmar las opciones disponibles, precio y tiempo de entrega.